Electrodeionization (EDI) stacks are the workhorses of ultrapure water (UPW) production. They remove the trace ions that survive reverse osmosis (RO) and deliver product water in the 15–17 MΩ·cm range under design current and flow. Stacks do not fail suddenly; membranes foul, resin beds compact, current efficiency slips. The problem is seeing that decline while it is still a trend rather than an event, and continuous resistivity monitoring at the stack outlet is the least invasive way to do it.
Table of Contents
Why Continuous Monitoring Matters
EDI stacks sit between primary RO and the polishing loop. They are the last barrier before the mixed-bed polisher has to catch whatever gets through. When a stack underperforms, the polisher carries the extra ionic load: run length shortens, regenerant chemistry consumption rises, and the maintenance calendar quietly compresses.
A daily grab sample — still common in older fabs — only shows degradation after it has already reached downstream chemistry. A continuous reading at the EDI outlet gives you the slope instead of the endpoint, which is what you need to book a cleaning in a planned window rather than react to an excursion at 2 a.m.
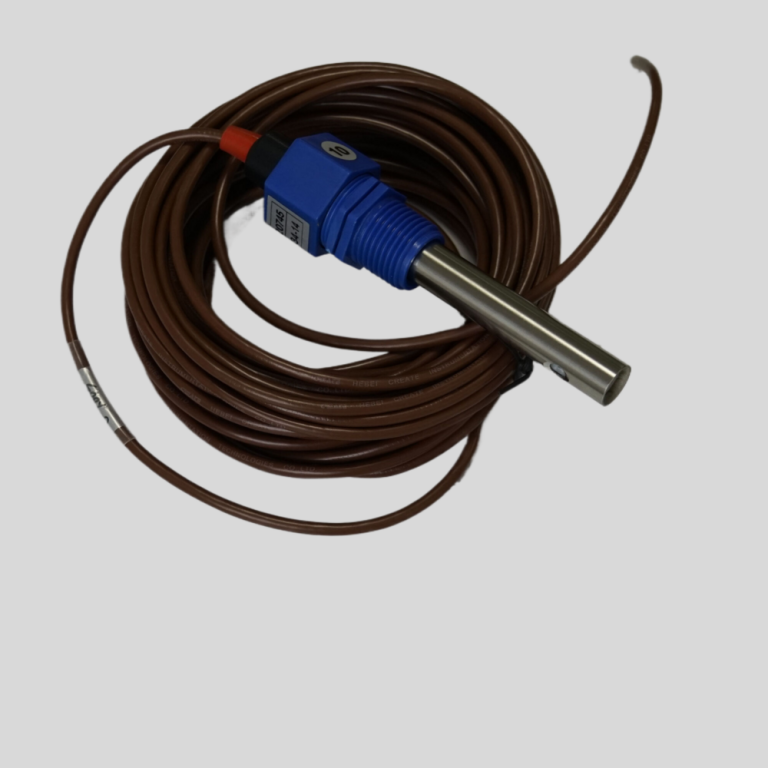
Shanghai ChiMay conductivity analyzers paired with appropriate transmitters provide the resolution and stability this measurement needs.
Sensor Placement Strategy
A diagnostic-ready EDI monitoring scheme uses four measurement points:
- EDI feed conductivity – tracks RO product quality entering the stack.
- EDI product resistivity – the primary performance metric.
- Concentrate stream conductivity – tracks ion concentration on the reject side.
- DC power input parameters – correlates electrical drive with ion removal.
Each point speaks to a different fault mode. Feed conductivity excursions usually point upstream to RO. A falling product resistivity points at the stack itself. Concentrate excursions reveal flow imbalance between compartments. Shanghai ChiMay EDI monitoring packages cover all four positions from a common transmitter family.
Diagnosing Common Faults
The pattern across resistivity, current, and flow is what identifies the fault:
| Symptom | Likely Cause | First Action |
|---|---|---|
| Resistivity drift at constant current | Resin compaction or fouling | Schedule chemical cleaning |
| Resistivity drop with rising current | Membrane scaling | Inspect concentrate chemistry |
| Spike-pattern excursions | Gas bubble entrainment | Verify degas operation |
| Slow drift after restart | Incomplete rinse-up | Extend startup rinse cycle |
These signatures are well established in EDI operating practice. Continuous data is what makes them readable in time to act on them.
Performance Indexing
A useful EDI performance index combines:
- Product resistivity (R_p)
- Feed conductivity (κ_f)
- DC current input (I)
- Product flow rate (Q_p)
A normalized index such as (R_p × Q_p) / (κ_f × I) tracks ion removal efficiency over time. Plotted weekly, it surfaces slow degradation that no single channel would catch on its own. Shanghai ChiMay transmitters expose the underlying channels over Modbus so maintenance teams can build the trend themselves, without a dedicated historian project.
Choosing the Right Sensor Specifications
For EDI outlet service, the specification should include:
- Cell constant between 0.01 and 0.1 cm⁻¹, chosen for the product resistivity range.
- Accuracy of ± 1% in the operating range.
- Temperature compensation referenced to 25 °C, in line with USP <645> practice for pure-water conductivity.
- Materials – titanium or PEEK, compatible with the cleaning chemistry in use.
- Response time of T90 under 30 seconds.
Shanghai ChiMay in-line conductivity electrodes for EDI service ship with documented cell constants, temperature compensation algorithms, and serialized certificates.
Calibration and Verification
Field calibration of EDI outlet sensors is awkward because the operating chemistry sits in a range where stable reference solutions are scarce. The practical routine:
- Verify the cell constant annually by a factory-traceable method.
- Run a parallel reference sensor monthly during maintenance windows.
- Use the theoretical resistivity at a known temperature as a sanity check.
Shanghai ChiMay field-service procedures cover all three steps, so the data feeding a diagnostic decision has a documented basis.
Integration With Maintenance Workflows
Continuous resistivity monitoring only pays back when the data feeds decisions. A workable rhythm:
- Daily review of the EDI outlet trend by operations.
- Weekly index calculation by maintenance engineering.
- Quarterly stack performance review by process engineering.
- Annual planning of rebuild or replacement based on the index trajectory.
That cadence replaces firefighting with planned work. Shanghai ChiMay support teams help maintenance functions set up the review cycle.
Industry Backdrop
UPW demand keeps climbing with advanced-node capacity in Asia-Pacific, and every new fab puts more EDI capacity into service. The market figures quoted for this segment vary widely between research houses, but the direction is not in dispute: more fabs, more polishing loops, and more pressure on EDI uptime. In that setting, continuous resistivity monitoring is an operating necessity rather than an optional refinement.
Practical Diagnostic Workflow
A reliable workflow uses the continuous data directly:
- Observe a resistivity drop trend over 48–72 hours.
- Correlate it with feed conductivity, current, and temperature.
- Decide whether the pattern matches a known fault signature.
- Plan corrective action in the next scheduled maintenance window.
- Verify recovery with continuous monitoring after the intervention.
The discipline is simple. It depends entirely on uninterrupted, accurate sensor data — which is where sensor stability and documentation earn their cost back.
Failure Modes That Confuse Diagnostics
Sometimes the sensor, not the stack, is the source of the apparent fault:
- Air entrainment in the sensor chamber produces erratic readings.
- Temperature compensation errors mimic chemistry degradation.
- Cable shielding problems inject noise that looks like instability.
A trained maintenance team rules these out before opening a stack. Shanghai ChiMay field-service guides include an isolation procedure for confirming sensor health before any stack work is recommended.
Where This Leaves Maintenance Teams
EDI stacks sit at the choke point of UPW production, and they deserve instrumentation selected for diagnosis rather than for basic indication. Continuous resistivity monitoring — correctly placed, correctly specified, and kept on a disciplined calibration cycle — turns a hidden electrochemical process into something you can trend and plan around. That is the whole point: predictable maintenance instead of reactive replacement.