The Short Version:
– Well-optimized electrochemical treatment systems can run at <2 kWh/m³ while holding >95% removal of target organic pollutants
– Energy is the largest operating cost in electrochemical treatment—commonly half or more of total operating expense—which is exactly why it rewards optimization
– Electrode material choice and pulsed power operation each contribute meaningful reductions versus conventional DC operation
– Shanghai ChiMay online analyzers provide the real-time data that energy optimization algorithms run on
Energy is the dominant operational cost component in electrochemical wastewater treatment, commonly representing 50-70% of total operating expense at typical electricity prices. The floor is set by treatment chemistry: complete mineralization of organic matter to carbon dioxide and water has a thermodynamic energy requirement on the order of a few kilowatt-hours per kilogram of COD, before a single real-world inefficiency is counted. Practical systems then stack overpotentials, solution resistance, and oxygen evolution on top, and the delivered energy per kilogram of COD rises accordingly. The saving grace is that treatment systems rarely need complete mineralization, and optimization strategies can cut energy consumption substantially while still meeting the treatment objective.
Table of Contents
Understanding Electrochemical Energy Consumption
Energy Requirement Fundamentals
The electrical energy required for electrochemical treatment depends on three primary factors:
Thermodynamic Requirement: The minimum energy needed to drive the oxidation reaction, set by the Gibbs free energy change of the oxidation reactions and the cell voltage those reactions imply.
Kinetic Requirement: Additional energy needed to overcome activation barriers and achieve practical reaction rates—overpotentials at the anode and cathode, solution resistance, and mass transfer limitations.
System Efficiency: The fraction of electrical energy that actually goes into pollutant oxidation versus losses to heat, oxygen evolution, and other side reactions.
Current efficiency quantifies system performance—the fraction of electrical charge that oxidizes pollutant versus competing reactions. Modern electrochemical systems achieve 70-85% current efficiency for organic oxidation, with the remainder lost to oxygen evolution and parasitic reactions.
Energy Consumption Calculation
For a wastewater stream with known COD concentration, energy consumption can be estimated:
Energy per Volume = (COD removed × Energy per mass COD) / Current efficiency
Example calculation for 95% COD removal from wastewater with initial COD of 2,000 mg/L:
- COD removed: 1,900 mg/L = 1.9 kg/m³
- Energy per kg COD: 2.0 kWh/kg (practical value for the system in question)
- Current efficiency: 75%
- Energy consumption: 1.9 × 2.0 / 0.75 = 5.1 kWh/m³
For higher removal efficiency (99%):
- COD removed: 1,980 mg/L = 1.98 kg/m³
- Energy consumption: 1.98 × 2.0 / 0.75 = 5.3 kWh/m³
The marginal energy cost of additional removal efficiency is modest when current efficiency holds up. The bigger lever is improving current efficiency and cutting overpotentials.
Optimization Strategies
Electrode Material Selection
Electrode material changes energy consumption through its effect on the oxygen evolution overpotential—the primary competing reaction. Materials that hold oxygen evolution at higher potentials maintain selectivity for organic oxidation even at higher cell voltages.
Dimensionally Stable Anodes (DSAs): Titanium anodes coated with mixed metal oxides (iridium-tantalum, ruthenium-iridium) are the workhorse of industrial electro-oxidation, running organic oxidation efficiently at cell voltages of 4-6 V with current efficiency for organic oxidation reaching 80-85% at optimized coating compositions.
Boron-Doped Diamond (BDD): BDD anodes hold the oxygen evolution potential well above 2.3 V vs. SHE—the highest among commercially available materials—which is what gives BDD its strong oxidative capability for recalcitrant organics. The trade-off is premium pricing and power supply systems with tighter requirements.
Where the research is heading: Coating chemistry is still moving. Newer iridium-based formulations continue to push the oxygen evolution overpotential down in laboratory reports, and every bit of that overpotential shows up directly in the energy bill. Treat any specific percentage improvement you read as lab-scale until it is demonstrated at yours.
Pulsed Power Operation
Conventional electrochemical treatment applies constant direct current (DC) to the electrode system. Pulsed power operation alternates between current application and rest periods, with several reported advantages:
Mass Transfer Enhancement: During rest periods, concentration gradients relax and fresh reactant diffuses back to the electrode surface. The next current pulse works against a higher reactant concentration, improving reaction rates.
Heat Management: Rest periods let the system cool, limiting the temperature rise that degrades electrode performance and drives cooling energy.
Energy Savings: Studies report 15-25% reduction in energy consumption with pulsed operation versus continuous DC at equivalent treatment efficiency. Optimal duty cycles—the ratio of current-on time to total time—fall in the 30-70% range depending on the wastewater.
Pulsed Waveforms: Square wave pulses at frequencies of 100-1,000 Hz are the practical band. Higher frequencies offer marginal benefit while adding power electronics complexity.
Optimized Cell Design
Electrode geometry and cell configuration change energy consumption through solution resistance and mass transfer:
Interelectrode Distance: Narrower spacing reduces solution resistance and the losses that come with it. Typical spacings of 5-10 mm balance energy efficiency against scaling and short-circuit risk.
Electrode Area to Volume Ratio: Higher area-to-volume ratios improve treatment capacity but raise capital cost. Optimal designs land around 30-50 m²/m³ for typical industrial wastewater applications.
Flow Regime: Turbulent flow enhances mass transfer, allowing higher current densities before mass transfer limitation sets in. Baffle designs and flow distributors create turbulent conditions through the reactor volume.
Practical Energy Benchmarks
Low-Concentration Wastewater (<500 mg/L COD)
For dilute streams, energy consumption is dominated by cell resistance rather than reaction thermodynamics:
- Typical consumption: 0.5-1.0 kWh/m³
- Target removal: 80-90% COD reduction
- Application: Textile dyeing rinse water, food processing effluents
Medium-Concentration Wastewater (500-2,000 mg/L COD)
This is the sweet spot for electrochemical treatment, where energy consumption balances against treatment efficiency:
- Typical consumption: 1.0-2.0 kWh/m³
- Target removal: 90-95% COD reduction
- Application: Chemical manufacturing, pharmaceutical production
High-Concentration Wastewater (>2,000 mg/L COD)
High-strength wastewater needs substantial energy for deep oxidation, but electrochemical treatment remains competitive with the alternatives:
- Typical consumption: 2.0-4.0 kWh/m³
- Target removal: 95-98% COD reduction (often combined with biological treatment)
- Application: Petrochemical, pulp and paper, landfill leachate
Worked Example: Industrial Wastewater Treatment
The following is an illustrative example built around a typical specialty chemicals application; the arithmetic is what matters for your own screening:
Facility Profile
A specialty chemicals facility processes 200 m³/day of wastewater with COD of 1,500 mg/L. The discharge permit requires <500 mg/L COD (67% removal target).
System Configuration
- Reactor volume: 25 m³ (two reactors in series)
- Electrode material: Iridium-tantalum DSA on titanium substrate
- Electrode area: 750 m² total (both reactors)
- Power supply: Pulsed DC with programmable duty cycle
- Monitoring: Shanghai ChiMay online COD analyzer for process control
Operating Results
After optimization, the system achieved stable operation at:
- Influent COD: 1,450-1,550 mg/L
- Effluent COD: 350-450 mg/L
- Removal efficiency: 73-78%
- Energy consumption: 1.4-1.6 kWh/m³
- Current efficiency: 78-82%
Optimization Interventions
Several interventions, applied together, brought energy consumption down from an initial 2.1 kWh/m³ to ~1.5 kWh/m³:
- Pulsed power implementation: 50% duty cycle at 500 Hz
- Electrode spacing optimization: reduced from 12 mm to 7 mm
- Current density optimization: reduced from 20 to 12 mA/cm²
- Automated control based on online monitoring: trims current density whenever the COD analyzer shows the effluent is comfortably below target
Economic Impact
At an electricity price of $0.21/kWh, the numbers work out as follows for a 200 m³/day train:
- Annual energy (before, 2.1 kWh/m³): 200 × 2.1 × 365 ≈ 153,000 kWh → ≈ $32,000/yr
- Annual energy (after, 1.5 kWh/m³): 200 × 1.5 × 365 ≈ 110,000 kWh → ≈ $23,000/yr
- Annual savings: ≈ $9,000 per 200 m³/day of capacity — savings scale linearly with throughput
For this size of installation the optimization work paid for itself inside the first year; on a multi-train site the same percentage savings carry proportionally more weight.
Monitoring for Energy Optimization
Shanghai ChiMay Online Analyzers
Effective energy optimization requires continuous monitoring of treatment performance to drive dynamic parameter adjustment:
COD/TOC Analyzers: Provide real-time treatment efficiency data for current density optimization. When treatment efficiency runs ahead of target, current density can be trimmed to save energy.
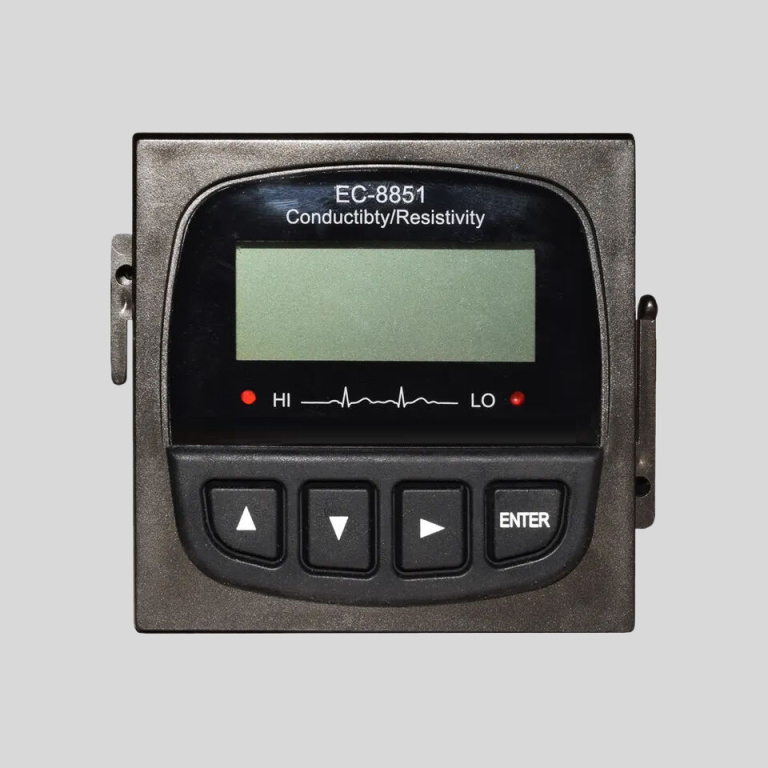
Conductivity Sensors: Monitor electrolyte concentration, enabling optimization of supporting electrolyte addition. Excess electrolyte raises conductivity but adds chemical cost; too little raises resistance and energy consumption.
pH and ORP Sensors: Indicate treatment progress and endpoint. A rising pH and stabilizing ORP signal treatment completion, enabling automated power reduction.
Control System Integration
Modern electrochemical treatment systems integrate monitoring data with automated control:
Setpoint Optimization: Control algorithms continuously adjust current density based on online COD measurements, holding target removal efficiency at minimum energy consumption.
Predictive Control: Algorithms predict treatment requirements from influent characterization, enabling anticipatory adjustment of operating parameters.
Maintenance Scheduling: Monitoring data identifies electrode degradation and scaling, triggering cleaning cycles before energy consumption climbs.
Conclusion
Electrochemical wastewater treatment at <2 kWh/m³ energy consumption is achievable with current technology. Electrode material selection, pulsed power operation, and automated control built on continuous monitoring each take a bite out of energy consumption compared with conventional operation. Shanghai ChiMay online analyzers provide the measurement foundation for that optimization—treatment systems that meet their objectives while keeping operating cost down.